
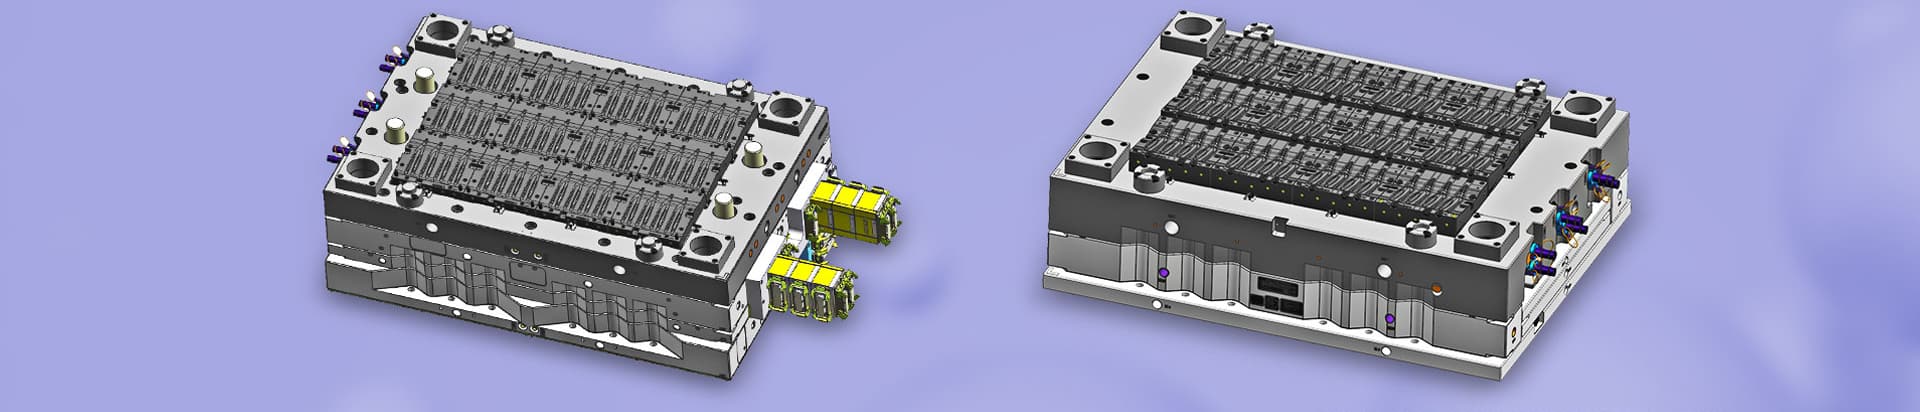
Various tools and products used in daily production and life, from machine bases, casings to casings of various household appliances, are closely related to molds. The shape determined by the production process of home appliance mold manufacturers determines the shape of these products, and the quality and precision of home appliance mold manufacturers also determine the quality of these products. Let us know about home appliance mould manufacturers China.
It mainly includes mold filling and pressure maintaining cooling port demoulding. The priming phase is the first step in the entire injection cycle. Time from appliance mold closure to the end of approximately 95% mold cavity filling. In theory, the shorter the filling time, the higher the molding efficiency, but in actual production, the molding time is affected by various conditions.
High-speed filling. The results show that the shear rate is large during high-speed filling, and the shear thinning effect reduces the viscosity of the plastic and reduces the overall flow resistance; local viscous heating reduces the thickness of the solidified layer. Therefore, in the flow control stage, the cooling effect of thin walls is not obvious due to high-speed filling, so the effect of rate is the upper hand.
Raise at low speed. The results show that the system has low shear rate, high local viscosity and large flow resistance. Due to the slow feeding speed and slow flow rate, the heat conduction effect is obvious, and the heat is taken away by the cold mold wall. With a small amount of viscous heating, the thickness of the solidified layer becomes thicker, further increasing the flow resistance of the thin-walled surface.
Generally speaking, the weld strength in the high temperature area is better. In addition, the temperature of the two melts in the high temperature zone is similar, and the thermal properties of the melts are basically the same, which increases the strength of the fusion zone; on the contrary, in the low temperature zone, the welding strength is poor.
It is the continuous application of pressure to compact the melt and increase the density of the plastic to compensate for the shrinkage behavior of the plastic. During the pressure holding process, the back pressure is high because the cavity is filled with plastic. In the packaging and pressing process of home appliance mold manufacturers, the screw of the injection molding machine can only move slowly, and the flow speed of the plastic is relatively slow. At this time, this flow is called packing flow.
Due to the cooling of the home appliance mold wall, the plastic solidifies rapidly, and the melt viscosity increases during the heat preservation stage, and the resistance in the mold cavity is very large. In the later stage of packing, the plastic part is gradually formed. This stage should continue until the nozzle is solidified and sealed. At this point, the cavity pressure reaches the highest value during the filling phase. During the filling stage, the plastic exhibits partial compressibility due to high pressure.
In the high pressure area, the plasticity is relatively dense and the density is high; in the low pressure area, the plasticity is loose and the density is low. The density distribution varies with time and location. During the filling process, the plastic flow velocity is very low and the flow does not play a dominant role. Pressure is the main factor affecting the filling process. During the filling process, the cavity is filled with plastic, and the gradually solidified melt is used as a medium for transmitting pressure.
The pressure in the mold cavity is transmitted to the surface of the mold wall through the plastic, making the home appliance mold easy to open. Therefore, proper clamping force is required for mold clamping.




 Call us on:
 Email Us:
 1st Floor, Block1, No.3 Beiting Road, Houting Community, ShaJing Street, Bao'An District, Shenzhen City, Guangdong Province, China
 English
 Deutsch
 italiano
 русский
 français
 română
 العربية
 Español
 Polska
 日本語
 한국어
